
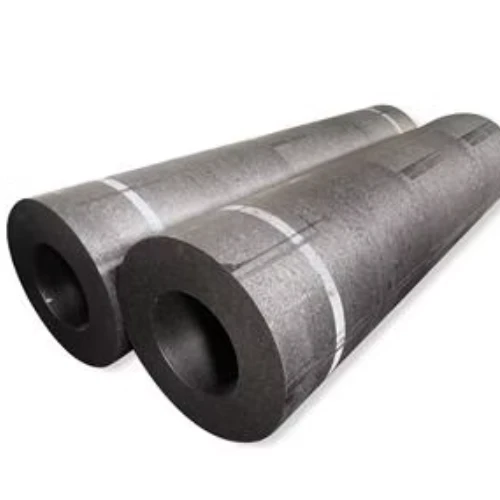


Hebei Fengchao Import and Export Co., Ltd. is one of the most reliable manufacturers and suppliers of graphite edm electrodes in China. With a professional production team, we are able to meet the needs of the majority of our customers. If you're going to wholesale bulk graphite edm electrodes made in China, welcome to get pricelist from our factory.
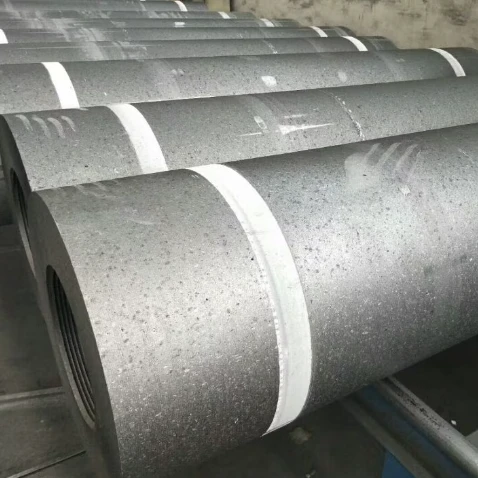
Our quasi-ultra-high-power graphite electrodes for electrical discharge machining (EDM) feature a dense and homogeneous internal texture with strictly controlled impurity content. They deliver stable and uniform spark output under fluctuating discharge energy conditions, reducing the probability of arc scratch defects on the surface of mold cavities. Balancing premium machining performance and material cost advantages, this grade supports both high-stock roughing and high-definition finishing of complex mold cavities. It provides a practical mid-to-high-end solution for mold manufacturing workshops aiming to boost EDM efficiency while controlling consumable expenditure.
Quasi-ultra-high-power EDM graphite electrodes adopt an optimized grain structure formula to enhance thermal spalling resistance under high-frequency pulse discharge conditions. They retain sharp edges and fine features during high-intensity spark erosion machining and greatly reduce the risk of edge chipping. They perform steadily in continuous repeated EDM of multi-cavity molds and are widely used to machine complex cavities of precision plastic injection molds and high-pressure die-casting molds. Suitable for mold prototyping and medium-batch mold production, they help mold makers shorten mold trial cycles and stabilize the machining quality of molded mold surfaces.
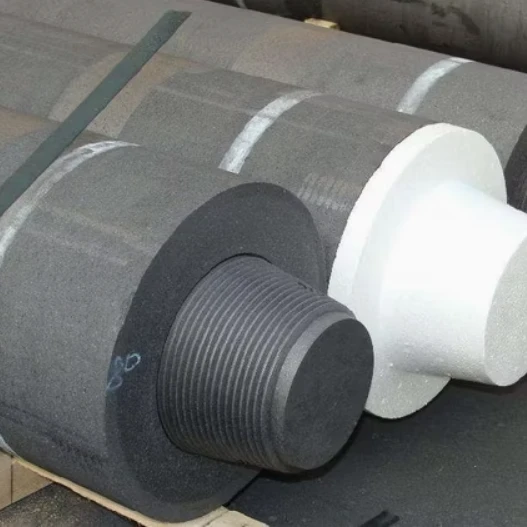
Quasi-ultra-high-power EDM graphite electrodes are produced from graded fine-grain calcined coke via the cold isostatic pressing process. Rigorous metallographic and physical property inspections guarantee excellent isotropy, and custom-machined EDM electrodes can be supplied for mold customers.
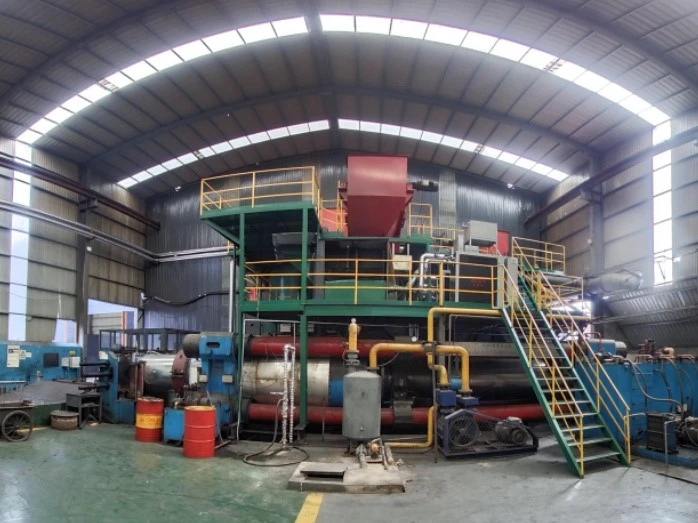
Factory Tour
FAQ
Q: How do machining parameters affect the actual wear rate of quasi-ultra-high-power EDM graphite electrodes?
A: The electrode wear ratio is closely related to pulse on-time and peak current. Appropriately extending the pulse on-time can reduce the relative graphite wear; excessively high peak current accelerates edge erosion. It is recommended to gradually adjust discharge parameters according to cavity depth instead of directly applying the machine's maximum settings.
Q: If customers machine finished electrodes from graphite blanks on their own, what finishing allowance is recommended?
A: A finishing allowance of 1.5–3 mm is recommended for blanks. Insufficient allowance tends to expose tiny subsurface pores after milling; excessive allowance prolongs CNC machining time and accelerates cutter wear.
Q: What precautions should be taken when clamping EDM graphite electrodes on the machine spindle?
A: Clamping pressure must not be excessive. Although this graphite has good mechanical strength, over-tight clamping generates invisible internal microcracks. These microcracks propagate under subsequent discharge thermal shock and may cause local chipping and detachment of the electrode.
Q: How should EDM graphite electrodes be cleaned before mounting after CNC milling?
A: Blow away fine graphite dust with dry compressed air. Direct water rinsing is prohibited. Residual moisture trapped inside pores leads to unstable sparks and intermittent arcing during discharge.
Q: Are there performance differences when machining this graphite grade using kerosene dielectric versus deionized water as the discharge medium?
A: Material removal rate is higher in deionized water, yet the relative electrode wear also increases. Oil-based dielectric facilitates finer mold cavity surface finish. Discharge process parameters need to be re-adjusted after switching the dielectric medium.
Q: Can scattered micro-pores inside graphite blanks be completely eliminated by CNC milling?
A: Isotropic graphite inevitably contains sporadic micro-pores. If micro-pores lie just beneath the finished machined surface, they will be exposed after milling. For ultra-precise cavity machining, it is recommended to select a higher-density grade or moderately increase the finishing allowance.
Hot Tags: graphite edm electrodes, China graphite edm electrodes manufacturers, suppliers, factory